
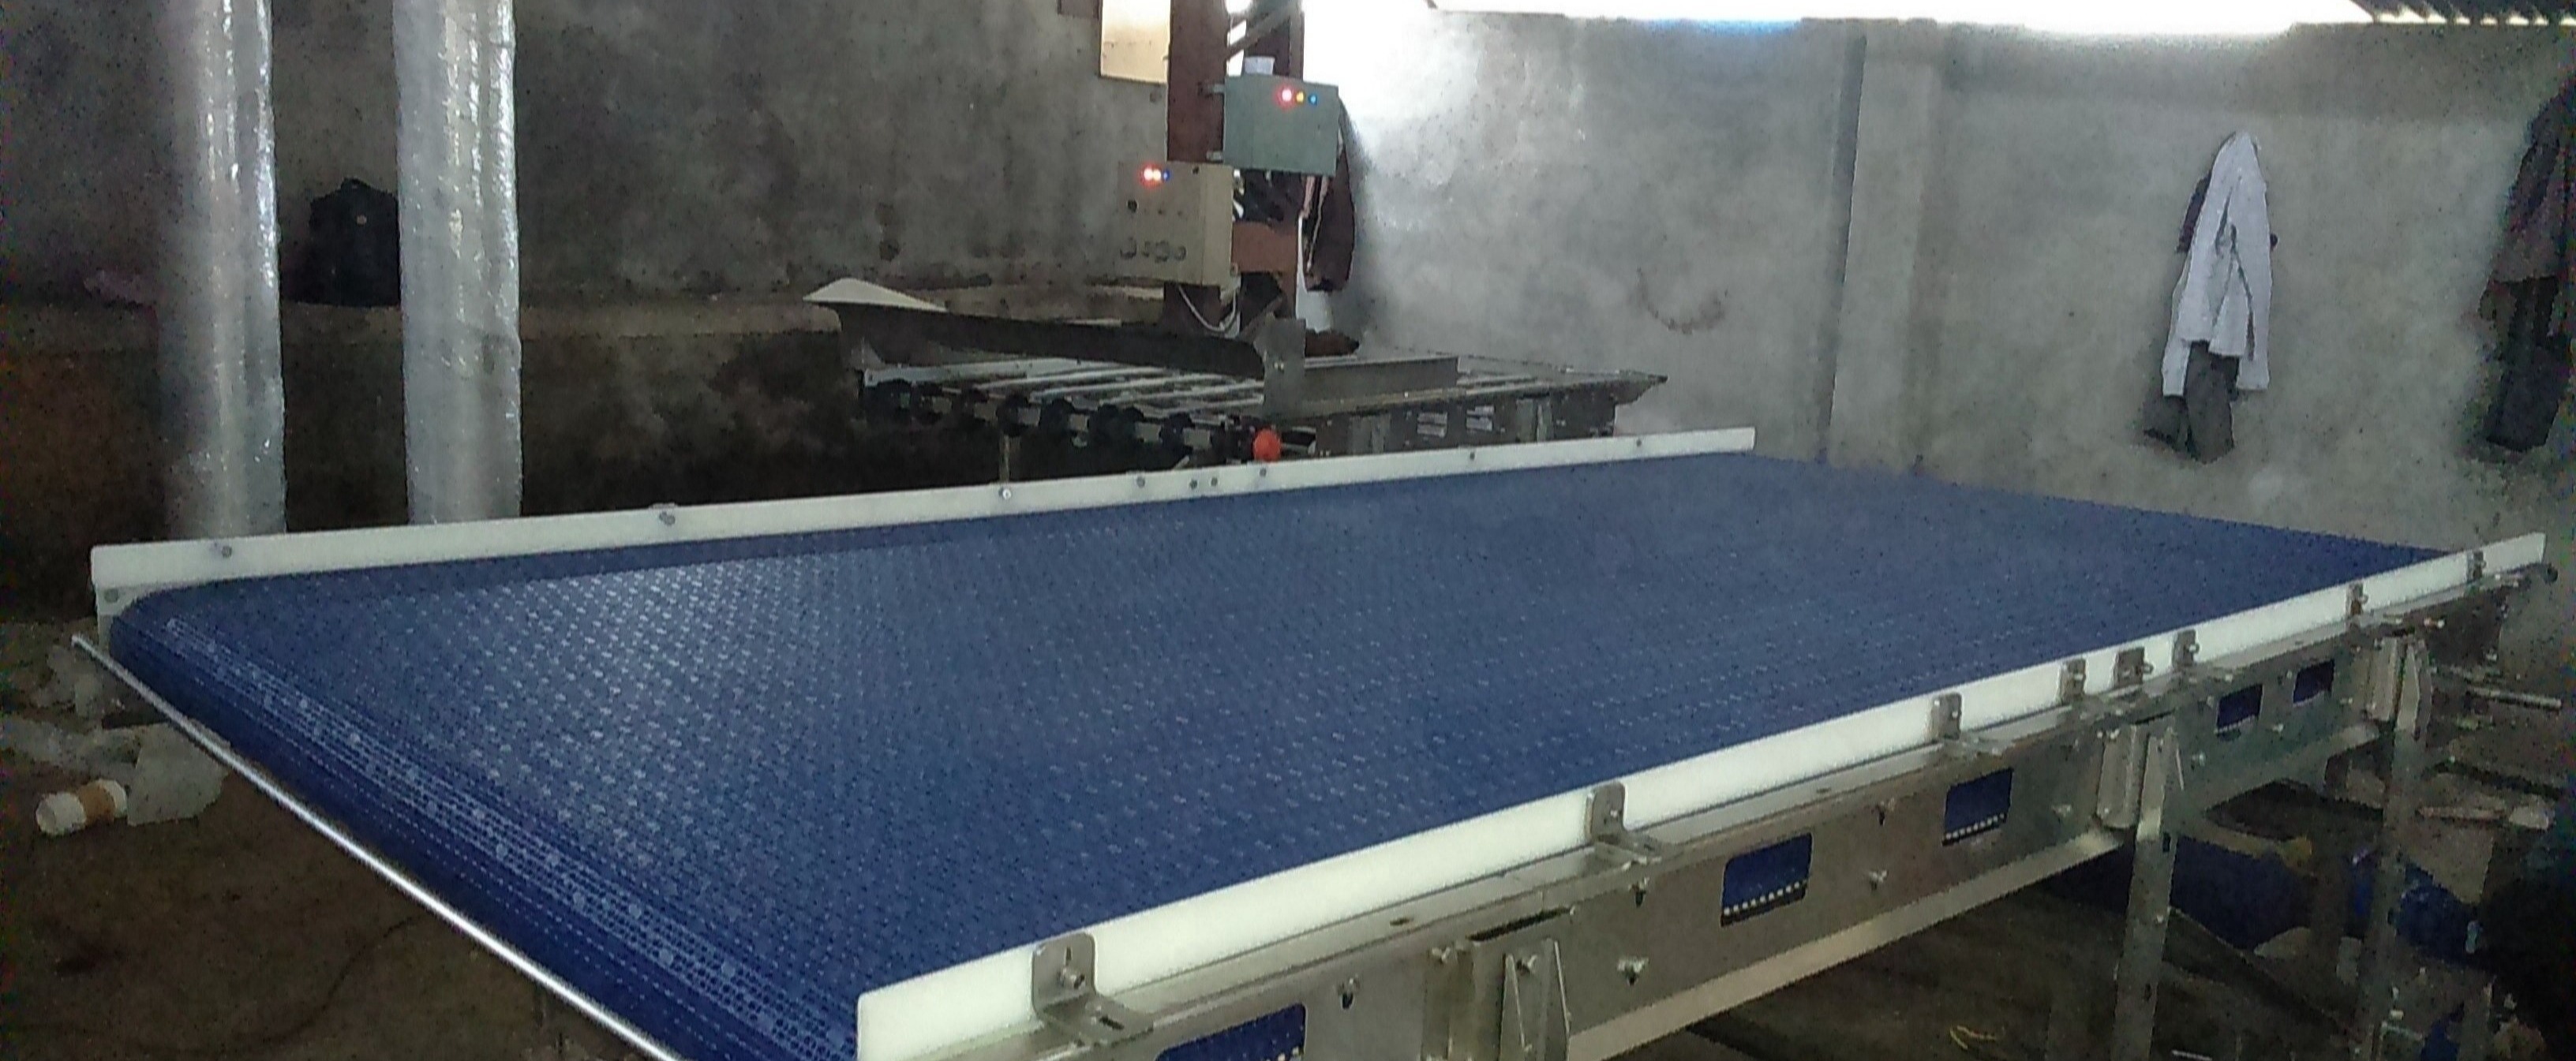
Efficient material movement is essential for modern manufacturing facilities. Industries handling bulk materials, powders, aggregates, food products, minerals, and industrial waste require reliable transportation systems to maintain smooth production. A Belt Conveyor Manufacturer helps businesses design and implement conveyor solutions suitable for their specific operational requirements.
Across the United Kingdom, industries are increasingly focusing on improving internal material flow, reducing manual handling, and increasing production efficiency. Properly designed conveyor systems play an important role in achieving these objectives.
Understanding Industrial Belt Conveyor Systems
A belt conveyor is a mechanical material handling system designed to transport materials continuously from one location to another. These systems are widely used because they provide consistent movement and can be customised according to plant requirements.
Common applications include:
Bulk material transportation
Food processing operations
Mining and mineral handling
Chemical processing plants
Packaging industries
Biomass handling facilities
The design of the conveyor depends on the material type, distance, capacity, and operating environment.
Choosing The Right Conveyor Design
Different materials require different conveyor configurations. A system designed for food products may have different requirements compared to one used for heavy industrial materials.
Important selection factors include:
Material weight
Particle size
Moisture content
Required conveying distance
Operating speed
Inclination requirements
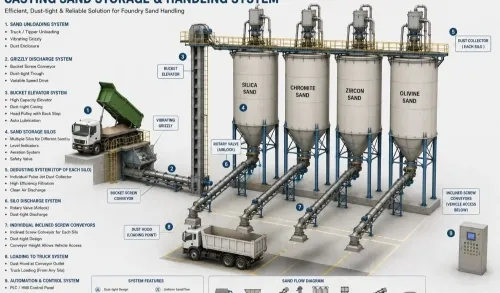
For example, a sand belt conveyor may require durability and resistance to abrasive materials, while a food belt conveyor may require designs focused on cleanliness and product protection.
Applications Of Belt Conveyors In Different Industries
Mining And Mineral Processing
Industries handling materials such as iron ore require strong conveyor systems capable of continuous operation. An iron ore belt conveyor manufacturer must consider heavy loads, wear resistance, and long operating cycles.
Food Processing
Food industries require controlled material movement systems that support hygiene standards and efficient production workflows.
Biomass Handling
Biomass materials often have unique flow characteristics. A biomass belt conveyor manufacturer needs to consider moisture levels, particle size, and handling requirements.
Improving Plant Efficiency Through Better Material Movement
An efficient conveyor system reduces unnecessary movement of materials and improves workflow throughout the facility.
Benefits include:
Reduced manual handling requirements
Improved production consistency
Better workplace safety
Increased operational efficiency
Easier integration with other equipment
A properly planned conveyor system can become an important part of the complete manufacturing process.
Customised Conveyor Solutions For Industrial Requirements
Every facility has different layout limitations and production needs. Standard conveyor designs may not always provide the best solution.
Custom engineering may involve:
Inclined conveyors
Heavy-duty belt systems
Specialised material handling arrangements
Integration with processing equipment
Metasis Equipments Pvt Ltd develops industrial equipment solutions including conveyors and material handling systems for different industries.
Selecting An Experienced Conveyor Partner
Choosing the right manufacturer requires understanding of both equipment design and industrial processes. A conveyor system should support current production needs while allowing future expansion.
For businesses across the United Kingdom, reliable material handling solutions can improve productivity and support efficient plant operations. Engineering-focused conveyor design helps industries create safer, smoother, and more organised production environments.