
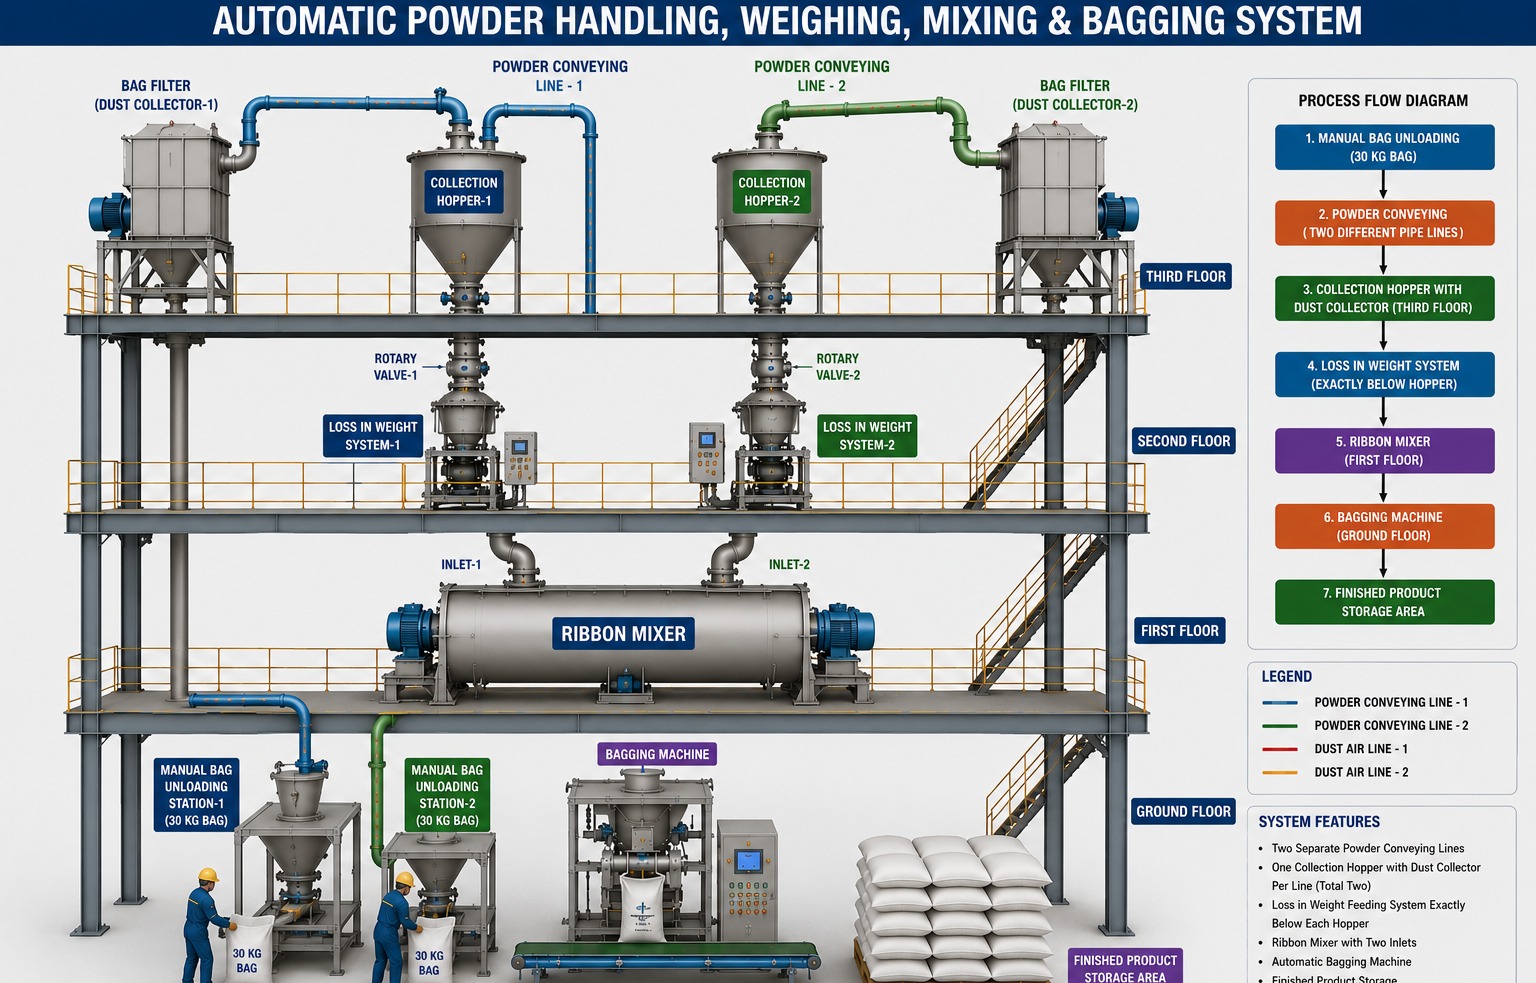
Efficient movement of raw materials and finished products is essential for smooth industrial operations. From manufacturing plants to food processing facilities, the way materials are transported, stored, and transferred can directly impact productivity, safety, and operating costs. Selecting the right material handling system supplier is therefore an important decision for businesses planning new facilities or improving existing production lines.
Industries across Australia depend on reliable material handling solutions for applications involving powders, bulk materials, chemicals, minerals, agricultural products, and packaged goods. A properly designed system reduces manual movement, improves workflow, and supports consistent production.
Understanding Industrial Material Handling Systems
A material handling system includes equipment and processes used to move materials throughout a facility. These systems are designed according to the type of material, production requirements, and plant layout.
Common material handling equipment includes:
Belt conveyors
Screw conveyors
Bucket elevators
Storage systems
Feeders
Mixers
Transfer systems
Each application requires a different engineering approach because materials behave differently during transportation.
Why Material Characteristics Matter
One of the most important aspects of material handling design is understanding the material being moved.
Engineers consider factors such as:
Particle size
Moisture content
Density
Flow characteristics
Temperature sensitivity
Corrosive properties
For example, food powders may require controlled handling to maintain hygiene, while mining materials may require heavy-duty systems designed for continuous operation.
Evaluating A Material Handling Supplier
Choosing a supplier involves more than checking available equipment. Businesses should evaluate whether the supplier understands the complete production process.
Important considerations include:
Engineering Experience
A supplier should be capable of designing solutions based on actual operational requirements rather than offering standard equipment without evaluation.
Customisation Capability
Industrial facilities often have unique layouts and production challenges. Custom-designed systems help improve efficiency and integration.
Process Understanding
Material handling equipment must work with other plant systems such as mixers, reactors, storage units, and production machinery.
Metasis Equipments Pvt Ltd provides engineering-based solutions for industrial equipment and material handling applications, focusing on customised systems designed around specific process requirements.
Applications Across Australian Industries
Mining And Minerals
Mining operations require robust handling systems for transporting materials such as iron ore and minerals over demanding routes.
Food Processing
Food industries require reliable systems for handling powders, ingredients, and bulk materials while maintaining cleanliness.
Chemical Manufacturing
Chemical plants need carefully designed handling solutions to manage powders, liquids, and process materials safely.
Agricultural Processing
Agricultural businesses often require solutions for grains, biomass, and other bulk materials.
Benefits Of A Well-Designed Handling System
A properly engineered material handling system can help businesses achieve:
Improved production efficiency
Reduced manual labour requirements
Better workplace safety
Lower material losses
More consistent operations
For industries in Australian regions such as Queensland, Western Australia, Victoria, and New South Wales, reliable material movement systems are essential for maintaining competitive operations.
Questions To Ask Before Finalising A Supplier
Businesses should consider:
Does the supplier understand the application?
Can the system be customised?
Does the design support future expansion?
Are maintenance requirements considered?
Can the equipment integrate with existing processes?
The right material handling system supplier helps businesses create a connected production environment where movement, storage, and processing work together efficiently.