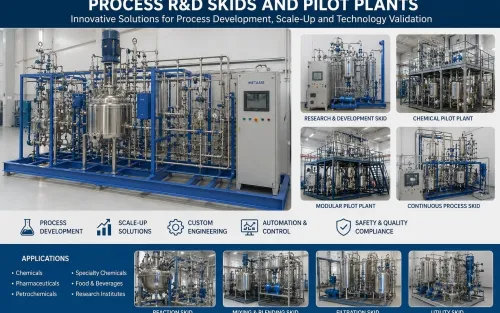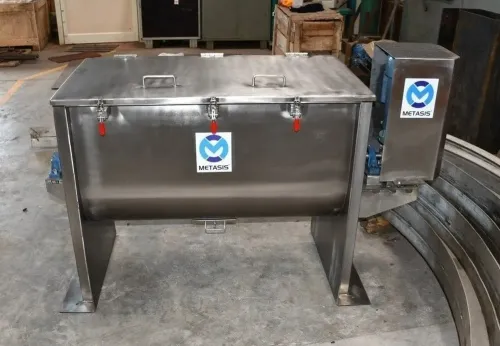

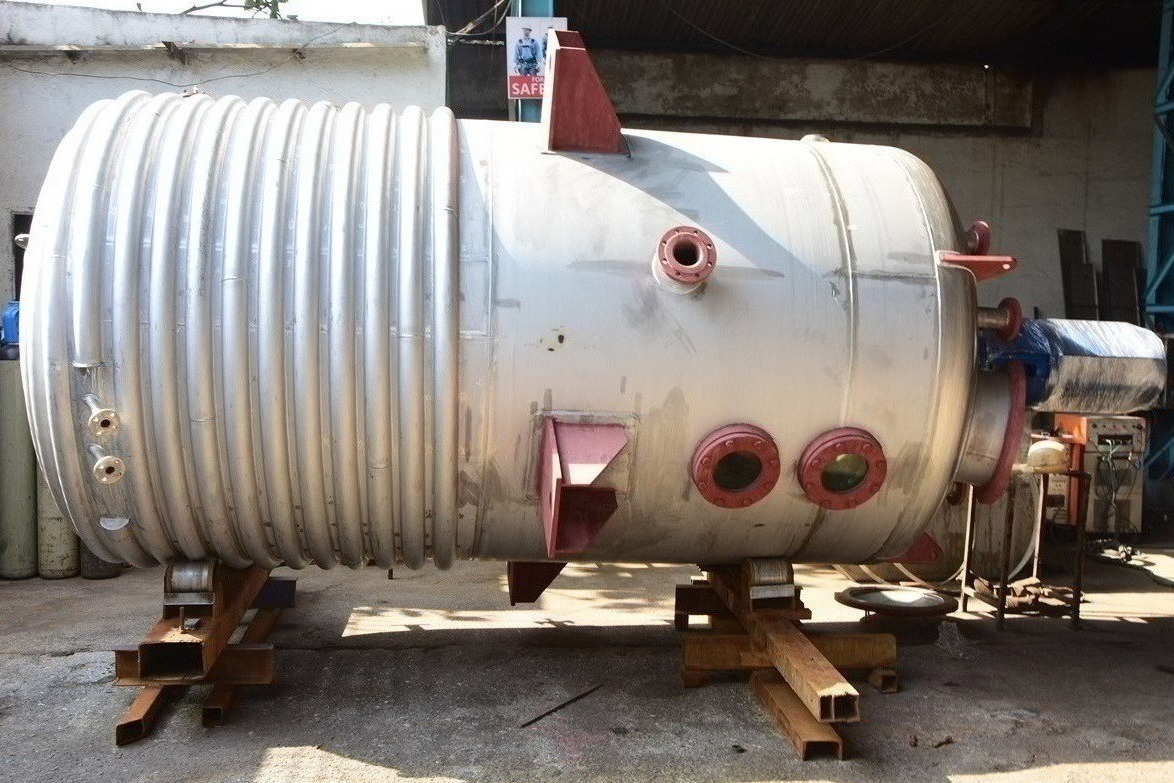
Chemical processing industries depend on accurately designed reaction systems to achieve consistent product quality and efficient production. A chemical reactor is one of the most important components in many manufacturing plants because it provides a controlled environment where chemical reactions take place.
A chemical reactor manufacturer develops reactor systems based on process requirements, material compatibility, operating conditions, and production capacity. Across the United States, industries such as chemicals, pharmaceuticals, specialty materials, and industrial manufacturing use customized reactors to support their production processes.
Selecting the correct reactor requires more than considering volume capacity. The design must match the specific reaction requirements and operating environment.
Understanding The Role Of Chemical Reactors In Manufacturing
Chemical reactors are designed to control important process parameters such as:
Temperature
Pressure
Mixing conditions
Reaction time
Material compatibility
The right reactor design helps manufacturers achieve consistent results while maintaining operational efficiency.
Different manufacturing processes may require different reactor configurations, including:
Batch reactors
Continuous reactors
Jacketed reactors
Agitated reactors
Pressure reactors
The selection depends on the application, production requirements, and characteristics of the materials being processed.
Factors To Consider Before Selecting A Chemical Reactor
Industries should evaluate several factors before investing in reactor equipment.
Important considerations include:
Type of chemical reaction
Required production capacity
Operating temperature range
Pressure requirements
Corrosion resistance
Mixing requirements
Cleaning and maintenance needs
For example, pharmaceutical applications may require precise control and hygienic design, while chemical manufacturing may require strong materials capable of handling demanding conditions.
Metasis Equipments Pvt Ltd provides engineering-based process equipment solutions for industries requiring customized manufacturing systems. The company focuses on developing equipment according to specific process requirements.
Importance Of Reactor Design In Process Efficiency
A properly designed reactor contributes to:
Better reaction control
Improved product consistency
Reduced processing issues
Efficient resource utilization
Safer operation
Poorly selected equipment can result in inconsistent production, increased maintenance requirements, or operational difficulties.
This is why engineering evaluation plays an important role before reactor installation.
Applications Of Industrial Reactors
Chemical reactors are used across multiple industries, including:
Chemical Manufacturing
Used for producing specialty chemicals, intermediates, and industrial products.
Pharmaceutical Production
Supports controlled reactions for drug-related manufacturing processes.
Food And Specialty Processing
Used in applications requiring controlled mixing and processing conditions.
Research And Development
Supports testing and scaling of new formulations and processes.
Supporting Scalable Manufacturing Growth
Growing industries require equipment that can support both current production needs and future expansion. Reactor systems should be designed with flexibility, maintenance accessibility, and operational reliability in mind.
For businesses across the United States planning new production facilities or upgrading existing systems, selecting an experienced chemical reactor manufacturer helps create reliable process solutions that support long-term manufacturing goals.