
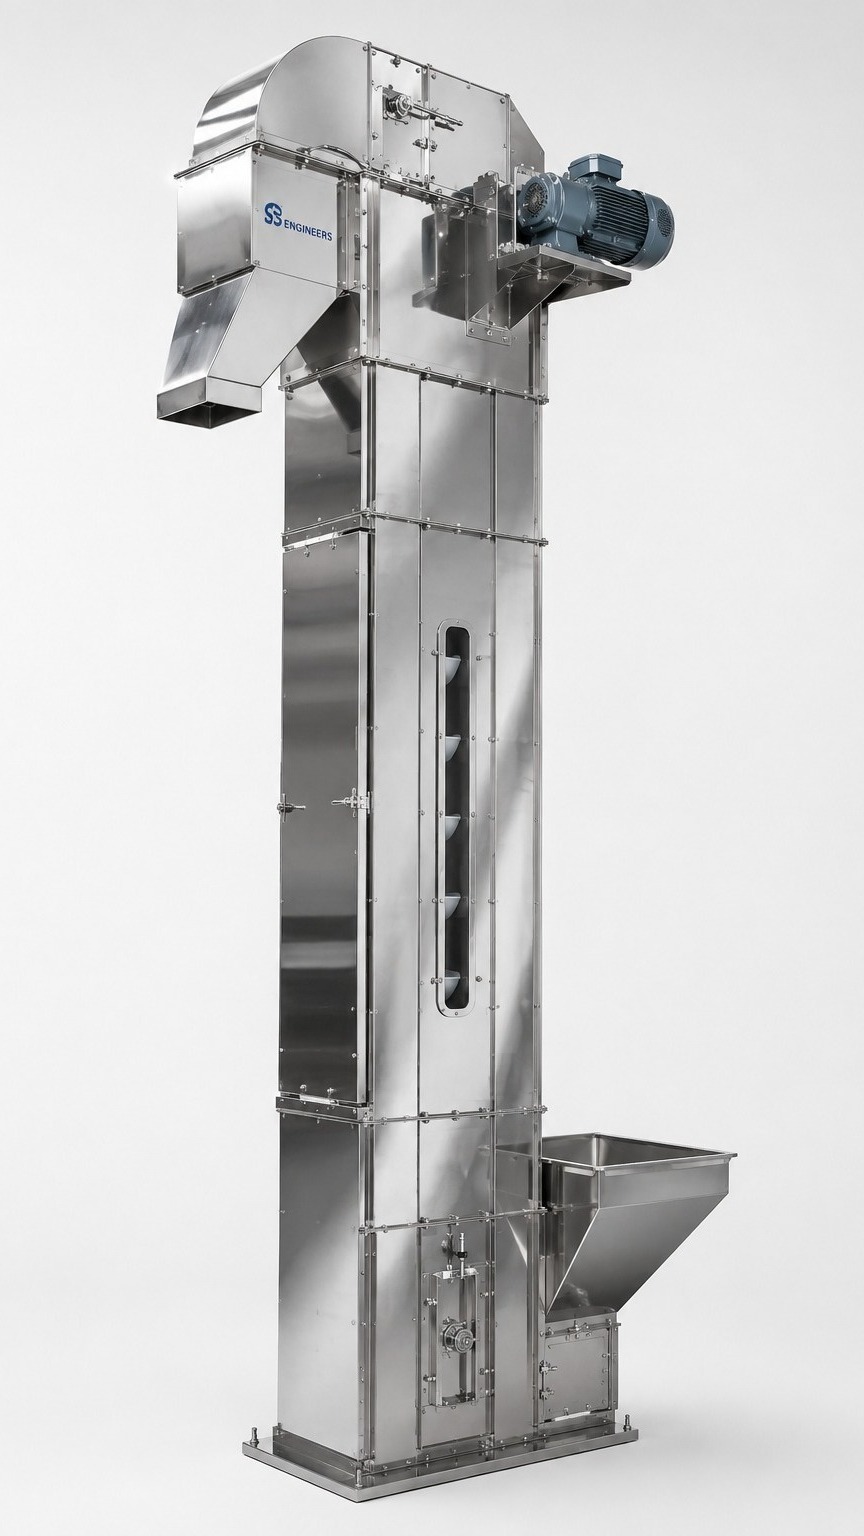
Many industries require efficient solutions for moving bulk materials vertically within processing facilities. When floor space is limited or materials need to be transferred between different production levels, bucket elevator systems provide a practical approach.
A bucket elevator manufacturer develops vertical conveying systems designed to lift materials safely and efficiently. Across the United States, industries including agriculture, food processing, cement, chemicals, and bulk material handling use bucket elevators for continuous vertical transportation.
Bucket elevators are commonly used for handling:
Grain materials
Powders
Granules
Minerals
Agricultural products
Industrial bulk materials
The design of the elevator depends on the material characteristics, required capacity, lifting height, and operating environment.
How Bucket Elevator Systems Work
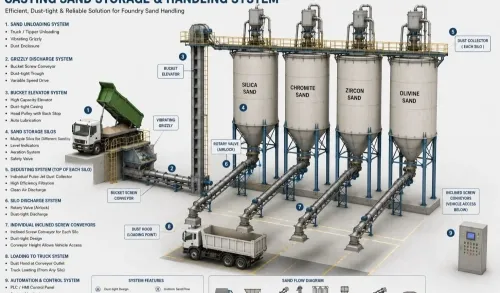
A bucket elevator uses a series of buckets attached to a rotating belt or chain mechanism. These buckets collect material from the lower section and transport it vertically before releasing it at the required discharge point.
The system includes important components such as:
Buckets
Belt or chain mechanism
Drive system
Casing structure
Feeding arrangement
Discharge system
Each component must be designed according to the application to ensure reliable operation.
Selecting The Right Bucket Elevator For Industrial Needs
Different industries have different requirements. A food processing facility may require equipment designed for product safety and cleanliness, while heavy industries may require robust systems capable of handling abrasive materials.
Businesses should evaluate:
Material density
Moisture content
Required capacity
Vertical height
Operating frequency
Maintenance requirements
For industries requiring high-volume material movement, proper selection helps reduce downtime and improves process efficiency.
Metasis Equipments Pvt Ltd provides industrial equipment solutions for material handling and process applications. The company focuses on developing customized systems based on specific manufacturing requirements.
Applications Of Bucket Elevators In Various Industries
Bucket elevators are widely used in:
Agricultural Processing
Used for grain, seeds, and biomass handling where vertical movement is required.
Food Manufacturing
Supports controlled transportation of powders, ingredients, and processed materials.
Chemical Industries
Helps move bulk materials safely within production environments.
Mineral And Industrial Processing
Handles heavy materials requiring durable conveying solutions.
Advantages Of Vertical Conveying Systems
A properly designed bucket elevator offers:
Efficient use of production space
Continuous material transfer
Reduced manual handling
Improved production workflow
Reliable bulk material movement
These benefits make bucket elevators valuable in facilities where efficient vertical transportation is required.
Planning For Reliable Material Handling
Choosing the right vertical conveying system requires understanding the complete production process. Factors such as material behavior, operating conditions, and future capacity requirements should be considered before installation.
For businesses across the United States planning industrial material handling improvements, working with an experienced bucket elevator manufacturer can help develop systems that support efficient and dependable production operations.