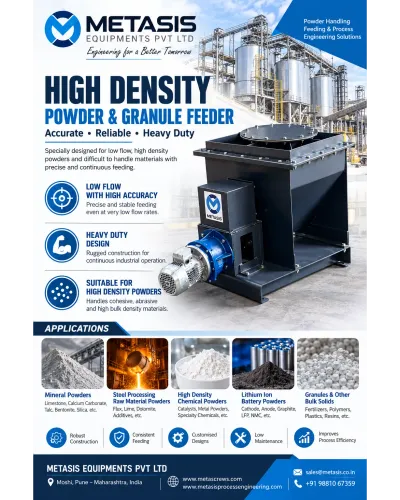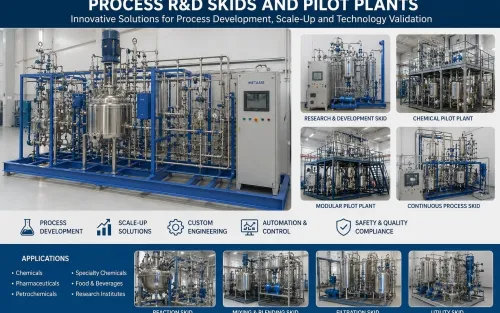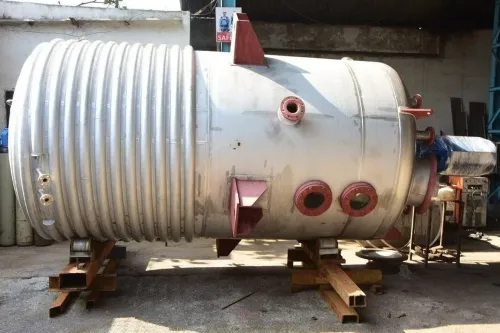

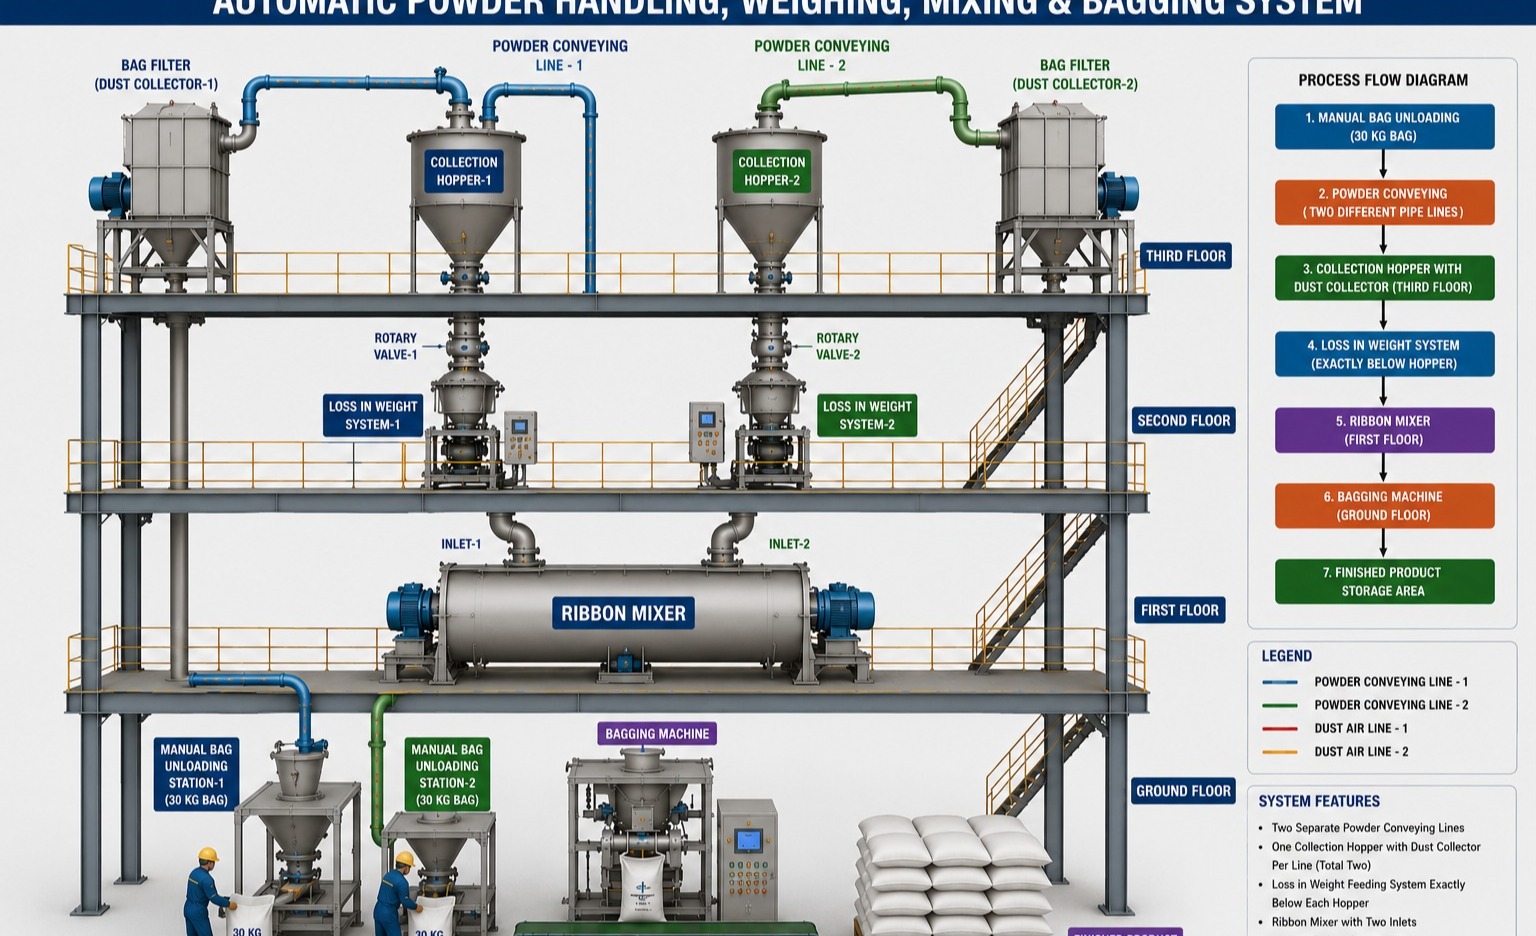
Efficient material movement is essential for industries that handle powders, bulk solids, chemicals, and processed materials. Poor material handling systems can create production delays, safety concerns, and unnecessary operational challenges.
A material handling system supplier provides engineered solutions that help industries transport, store, feed, and process materials efficiently. Across the United States, sectors such as food manufacturing, pharmaceuticals, chemicals, and industrial processing depend on customized handling systems.
Material handling systems may include:
Conveyors
Storage systems
Feeding equipment
Dosing systems
Mixing solutions
Transfer equipment
The right system depends on the type of material being handled and the requirements of the production process.
Importance Of Efficient Material Handling Design
Material handling is not only about moving products from one location to another. It involves maintaining product quality, reducing waste, and improving workflow.
A well-designed system helps businesses achieve:
Better production flow
Reduced manual handling
Improved workplace safety
Lower material losses
Consistent processing
For example, powder handling systems require careful design because fine materials may create challenges related to dust control, flow behavior, and accurate feeding.
Industry-Specific Material Handling Requirements
Different industries have different expectations from handling systems.
Food Processing
Food industries require solutions that support hygiene, contamination control, and product protection.
Pharmaceutical Manufacturing
Pharmaceutical facilities often need accurate powder handling, controlled transfer, and precise dosing systems.
Chemical Processing
Chemical industries require systems designed according to material properties, safety requirements, and environmental conditions.
Metasis Equipments Pvt Ltd develops engineering solutions for industrial applications involving process equipment, material handling systems, and customized manufacturing requirements.
Role Of Storage And Transfer Solutions
Storage systems are an important part of material handling operations. Businesses handling bulk materials require reliable storage solutions that maintain material quality and support continuous production.
Applications may include:
Chemical powder storage
Industrial liquid storage solutions
Bulk material storage
Casting sand storage systems
Proper storage design helps maintain smooth material flow between different production stages.
Improving Manufacturing Efficiency Through Better Systems
An integrated material handling approach connects different areas of production, reducing interruptions and improving overall efficiency.
Businesses should evaluate:
Material characteristics
Production volume
Required transfer distance
Automation requirements
Future expansion needs
This helps ensure the selected system supports long-term operational goals.
Building Reliable Industrial Processing Facilities
Modern manufacturing requires systems that are flexible, efficient, and designed according to specific applications. A reliable material handling system supplier helps industries create solutions that improve production performance while supporting operational safety.
For businesses across the United States involved in food, pharmaceutical, chemical, and industrial manufacturing, customized material handling solutions provide a foundation for efficient and dependable production operations.