A stopped biomass screw conveyor is not automatically safe: packed fibre, stored torque, hot bearings, methane and combustible dust can turn a routine jam into a serious incident. By following a controlled isolation, diagnosis, inspection and restart sequence, you can determine whether to clear the blockage in place or dismantle the conveyor.
Key takeaways
- Lock out power and release stored torque before opening the conveyor.
- Check for a mechanical jam before replacing the motor or drive.
- Clear biomass plugs with controlled methods, never by hand or reverse rotation alone.
- Restart empty at low speed and trace the material cause of the stall.
Make the Conveyor Safe Before You Investigate the Jam
A stopped motor does not mean a biomass screw is safe to open. A packed trough, raised gate or material column can keep torque on the flight and release it without warning.
- Stop the conveyor and all upstream feeders. Close slide gates or isolation valves so material cannot fall back into the trough or refill the inlet.
- Isolate and lock out the motor, variable-frequency drive, hydraulic pack and pneumatic actuators. Discharge electrical, hydraulic and pneumatic pressure, then test for zero energy with approved instruments.
- Prevent automatic or remote restart by isolating the control circuit and informing everyone working on connected equipment.
- Secure the screw against movement and verify zero shaft motion. Do not reach through an inlet, removed guard, cleanout door or inspection hatch, and do not probe the plug with a bar.
- Test the area for methane, hydrogen sulfide and oxygen deficiency before opening equipment at a bio-CNG material handling installation. Ventilate, control ignition sources and follow the site’s hazardous-area equipment rules.
- Treat hot bearings, combustible dust and stored torque as hazards during screw conveyor failure recovery. Release residual force only as the equipment manual and isolation procedure specify.
Do not reverse-jog, bar-turn or reset an overload while anyone is exposed to the screw. Confirm that the gearbox, coupling, backstop and flights are rated for reverse torque before considering controlled reverse operation.
Separate a Mechanical Jam from a Drive or Control Fault
A VFD trip code identifies where protection acted, not why the biomass screw conveyor stopped. Record the code, motor current, commanded speed and overload history before resetting anything. A stopped motor does not prove a clear shaft: a packed trough can hold torque in the flight.
After isolation and a documented zero-energy check, separate the drive from the conveyor only as the equipment procedure permits. Use the findings to locate the fault:
- No run command, failed proximity switch, open interlock or phase-loss indication points to the control or supply circuit.
- The VFD commands rotation, but the motor hums, trips immediately or shows abnormal current with the drive uncoupled: investigate the motor, terminals, insulation and brake.
- The uncoupled motor runs normally, but the gearbox output will not turn freely: investigate the coupling, gearbox, bearing or shaft.
- The output shaft turns, but the flight binds: look for a foreign object, compacted wet fibre, a bent flight, an overfilled inlet or material frozen in the trough.
- A broken coupling can leave the motor and VFD healthy while the screw remains stationary.
Do not keep jogging after a torque or current trip. Repeated low-speed attempts reduce motor cooling and can heat rubbing biomass. Check motor, gearbox and bearing temperatures, then record the obstruction location and trip evidence for the root-cause review.
Inspect the Drive, Bearings and Flight in the Right Order
Start at the drive end, not at the plug. Record the trip code, motor current and torque-limiter status, then isolate the drive from the screw and check whether the shaft turns freely by the approved method.
A free motor does not clear the conveyor: inspect the coupling, gearbox output shaft and gearbox oil before examining the rotating assembly.
Use this order during screw conveyor failure recovery:
- Check the coupling for sheared elements, displaced hubs or torsional cracking.
- Check the gearbox for abnormal oil, output-shaft movement and backlash.
- Check end bearings and hanger bearings for contamination, heat, seized movement or failed seals.
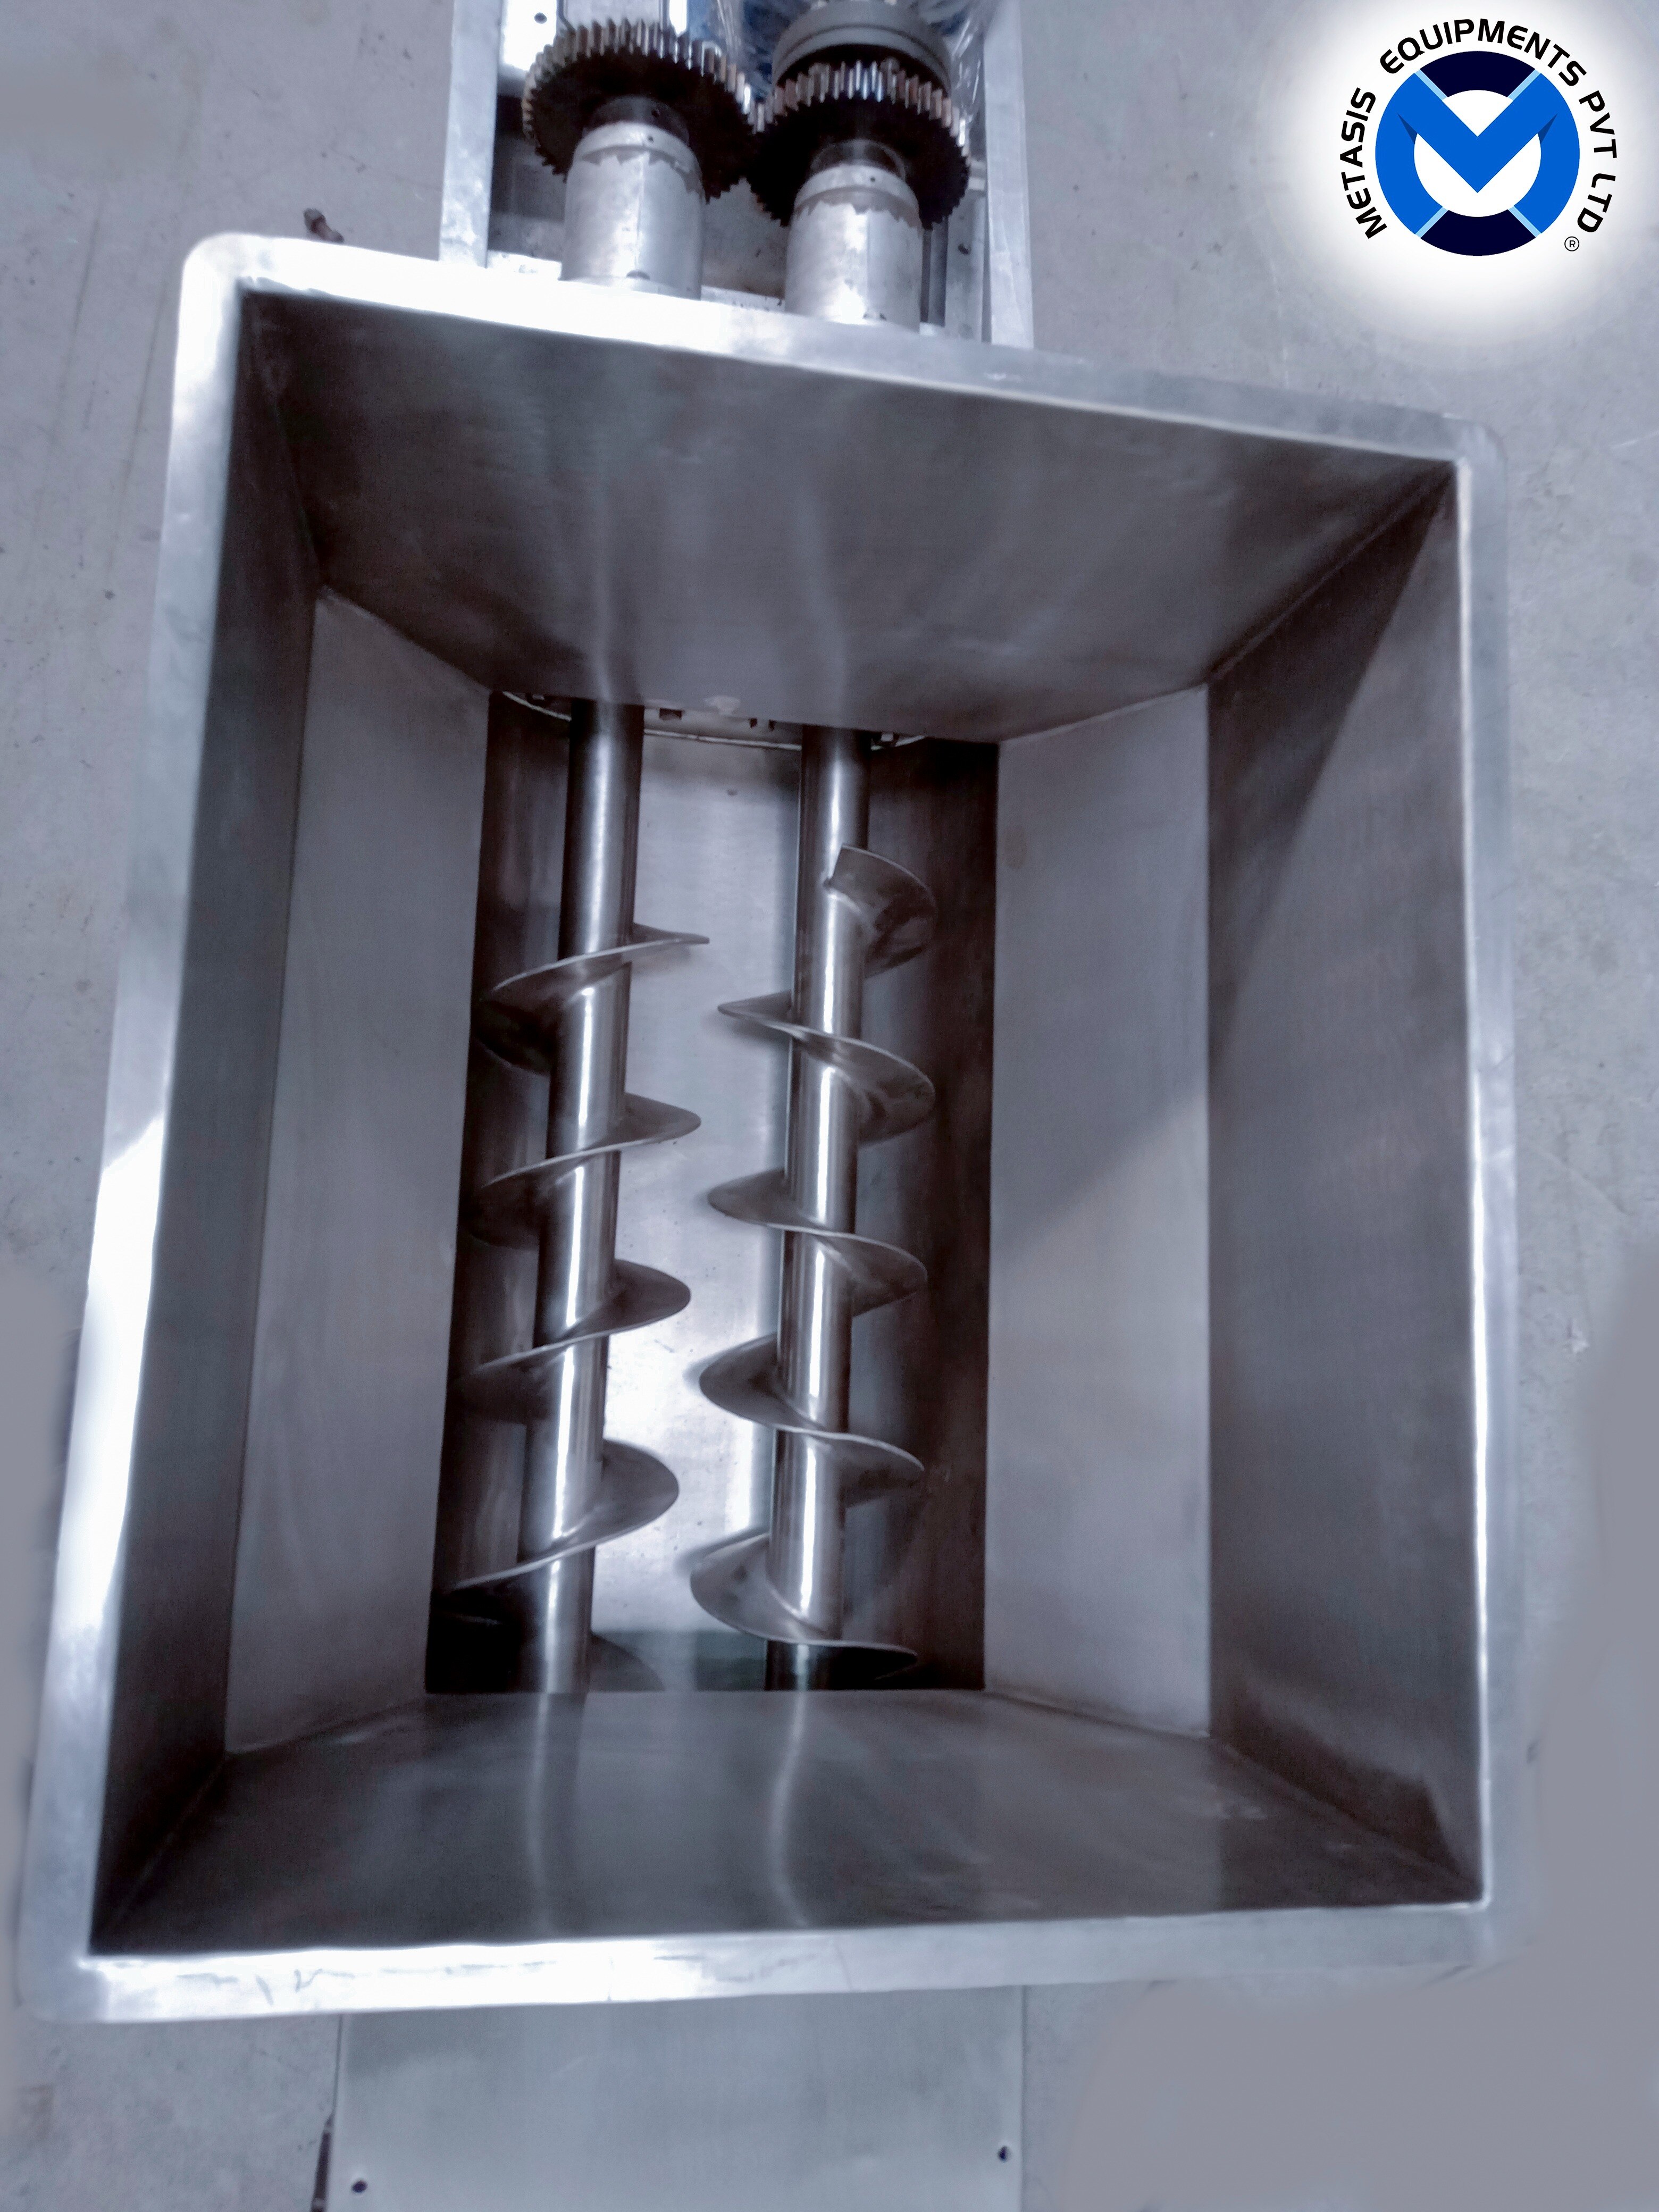
- Check shaft alignment, flight pitch, welds and flight-to-trough clearance through accessible sections.
- Check for a displaced hanger, packed inlet or plug at the discharge before authorising rotation.
| Component | Unsafe finding | Restart decision |
|---|---|---|
| Drive and coupling | Broken coupling, abnormal backlash or damaged backstop | Do not restart; repair and verify reverse-torque suitability |
| Bearings and shaft | Seized bearing, contamination, shaft bow or overheating | Do not restart; replace or realign before testing |
| Flight and trough | Contact marks, cracked welds, lost pitch or metal fragments | Do not restart; remove damaged parts and inspect downstream equipment |
Do not use reverse rotation as a shortcut. Confirm that the screw, coupling, gearbox and flights are rated for reverse torque; wrapped fibres can tighten, threaded parts can loosen, and a plug can move toward an unprotected inlet. A VFD restart cannot make rubbing, bent or cracked components safe.
Choose the Safest Method for Removing a Biomass Plug
Choose the method that removes stored material without putting a person near a moving shaft, sudden release or combustible dust cloud.
| Option | Use it when | Non-negotiable condition |
|---|---|---|
| Manual excavation | The plug is accessible through a cleanout and will not fall or shift | Lock out every energy source, verify zero movement, and use tools without reaching into a nip point |
| Controlled emptying | Material can leave through a discharge or low-point cleanout | Stop upstream feed, close gates, support covers, and collect the flow in a controlled container |
| Vacuum recovery | Fine, loose or combustible biomass can be extracted from a safe access point | Use a vacuum system rated for the dust hazard and suitable for the installation; never disperse dust with compressed air |
| Reverse rotation | Other methods cannot release the plug and the manufacturer permits reversal | Confirm the biomass screw conveyor, coupling, gearbox, flights and backstop are rated for reverse torque |
Treat reverse rotation as a recovery procedure, not a quick jog. It can tighten wrapped fibres, unscrew threaded parts, drive the plug toward an open inlet or damage the gearbox.
Do not probe through an inlet, hatch or removed guard while movement remains possible. Wet fibres can compact against the trough; dry fibres can bridge or wrap, so emptying the conveyor under control and restarting at low feed rate is safer than driving against a full plug.
Restart Gradually and Find the Biomass-Specific Root Cause
Treat screw conveyor failure recovery as a documented test, not a single restart. Test the screw empty at low speed, then introduce a small, controlled feed. Confirm smooth rotation, normal current, no rubbing, and stable bearing and gearbox temperatures before raising speed and feed in steps.
Do not flood the inlet: a full gate can recreate the plug before the repair is proven. In bio CNG material handling, repeat gas testing, ventilation and ignition-source controls must match the site’s hazardous-area classification before restart.
Record the evidence:
- Log material condition, including moisture, fibre length and visible contamination.
- Record feed rate, screw speed, motor current, trip code and torque-limiter status.
- Mark the obstruction location and document isolation steps before access.
- Describe damaged parts and capture the staged restart result.
Use those records to separate a foreign-object event from a repeatable process fault. Wet fibres or digestate compact in the trough and raise starting torque; dry fibrous feed can bridge the hopper or wrap the shaft.
Poor residence control from inlet flooding or unsuitable geometry can repeat the stall, while an undersized drive can trip under a normal loaded start. Correct the feed condition before increasing motor size.
Specify Recovery Features with a Screw Conveyor Manufacturer
Ask for a recovery-ready design package, not only a larger motor. It should define torque-limiter settings, overload trips, reverse-rotation limits, guarded cleanout access, emergency-stop locations, inspection interlocks, bearing-temperature monitoring and the safe method for removing a plug.
Request these records from the screw conveyor manufacturer:
- Screw diameter, pitch, flight thickness, trough clearance, shaft material, gearbox ratio, rated torque and permitted biomass moisture range.
- Motor-current limits, trip codes, torque-limiter status, coupling details and confirmation that every component tolerates controlled reverse torque.
- General arrangement drawings showing guards, cleanout doors, isolation points, backflow prevention and access around the inlet and discharge.
- Declaration of Conformity, operating instructions and the applicable Machinery Directive 2006/42/EC or Regulation (EU) 2023/1230 transition position.
- ATEX equipment category, marking, ignition-protection basis and interface limits under Directive 2014/34/EU.
- Recovery instructions covering lockout, dust-safe cleaning, inspection and restart testing.
For a French Bio-CNG site, align the package with the employer’s DUERP risk assessment, zone classification and site-specific DRPCE explosion-protection document. Record each stall’s feed rate, speed, current, trip code, plug location, damaged parts and restart result.
A screw conveyor manufacturer biomass France stalled conveyor search should lead to this evidence-based brief; Metasis Equipments Pvt Ltd can evaluate it without mistaking repeated stalls for motor failure.
Related products
 | Screw Conveyor Global Leader in Custom Screw Conveyor Solutions Metasis Equipments Pvt. Ltd. View product → |
 | Engineering Process System Automated Shredded Paddy Moisturizing System Automated Continuous Shredded Paddy Straw with Liquid Digestate Mixing & Supply System Advanced Feeding Solution for Bio-CNG and Biomass Extruder... View product → |
Frequently asked questions
What should you do before investigating a stalled biomass screw conveyor?
Isolate and lock out electrical power, control gates and other energy sources, then account for stored torque, gravity and material pressure before opening the conveyor.
How can you distinguish a mechanical jam from a drive or control fault?
Check the control circuit, motor status and drive alarms, then inspect whether the flight, trough or discharge path is physically blocked.
What is the safest way to remove a biomass plug?
Keep people clear of the conveyor, isolate all energy sources and use a controlled removal method suited to the plug, such as access doors, designed cleanout points or approved tools.
How should you restart a recovered screw conveyor?
Remove loose tools and guards only after inspection, restart empty at low speed, verify current and vibration, then introduce biomass gradually while monitoring the discharge.