Two stoppages in a defined operating period are enough to treat a blockage as a recurring failure, not an isolated upset. You will be able to separate mechanical jams from process-side plugging, collect the evidence a manufacturer needs, and judge whether the conveyor, its controls, or the material-handling arrangement requires redesign.
Key takeaways
- Treat two stoppages in 30 days or 100 operating hours as repeated blockage.
- Record feed rate, material condition, torque, location, and operating sequence for every event.
- Separate feed, conveyor geometry, material change, and mechanical-condition causes.
- Require a revised design basis and a documented blockage acceptance test.
Set a blockage threshold before you change the equipment
Treat two stoppages within 30 days or 100 operating hours as repeated blockage. Escalate any event that requires opening the trough to remove compacted material. This threshold turns vague screw conveyor blockage problems into a pattern worth testing, rather than a series of isolated operator interventions.
1. Record the date, material batch, throughput, screw speed, inclination, motor current, trip code, inlet level, discharge condition, and obstruction location. Time-correlate these details; a single motor-current reading cannot distinguish a feed surge from a restriction.
2. Investigate the complete process, not only the screw. Check for bridged or oversized feed, material entering before startup, excessive feed rate, incorrect rotation, worn or bent flights, inadequate clearance, and foreign objects. Record whether the conveyor started empty or full.
3. Inspect the discharge path. A partly closed valve, plugged chute, full receiving vessel, or poor venting creates back-pressure that can look like screw failure. Compare motor current with gearbox noise, torque-limiter trips, shaft deflection, bearing temperature, discharge flow, and upstream hopper level.
4. Do not fit a larger motor first after repeated overload trips. Extra torque can bend the shaft, break flight welds, damage bearings, or compact the blockage more tightly. An empty-running test proves only that the drive turns the shaft; it does not prove loaded capacity or full-load restart capability.
Use a safe, evidence-based investigation sequence
Before opening an access cover, isolate and lock out the screw conveyor, upstream feeder, hopper outlet, downstream valve, and every automatic restart logic. Verify zero electrical, pneumatic, hydraulic, gravitational, and stored-torque energy; trapped material or shaft torque can release without warning.
Record bulk density, moisture, particle-size distribution, temperature, feed rate, screw speed, operating hours, inclination, and whether the conveyor started empty or full.
- Inspect the inlet for bridging, flooding, an oversized lump, material present before startup, and incorrect feeder timing.
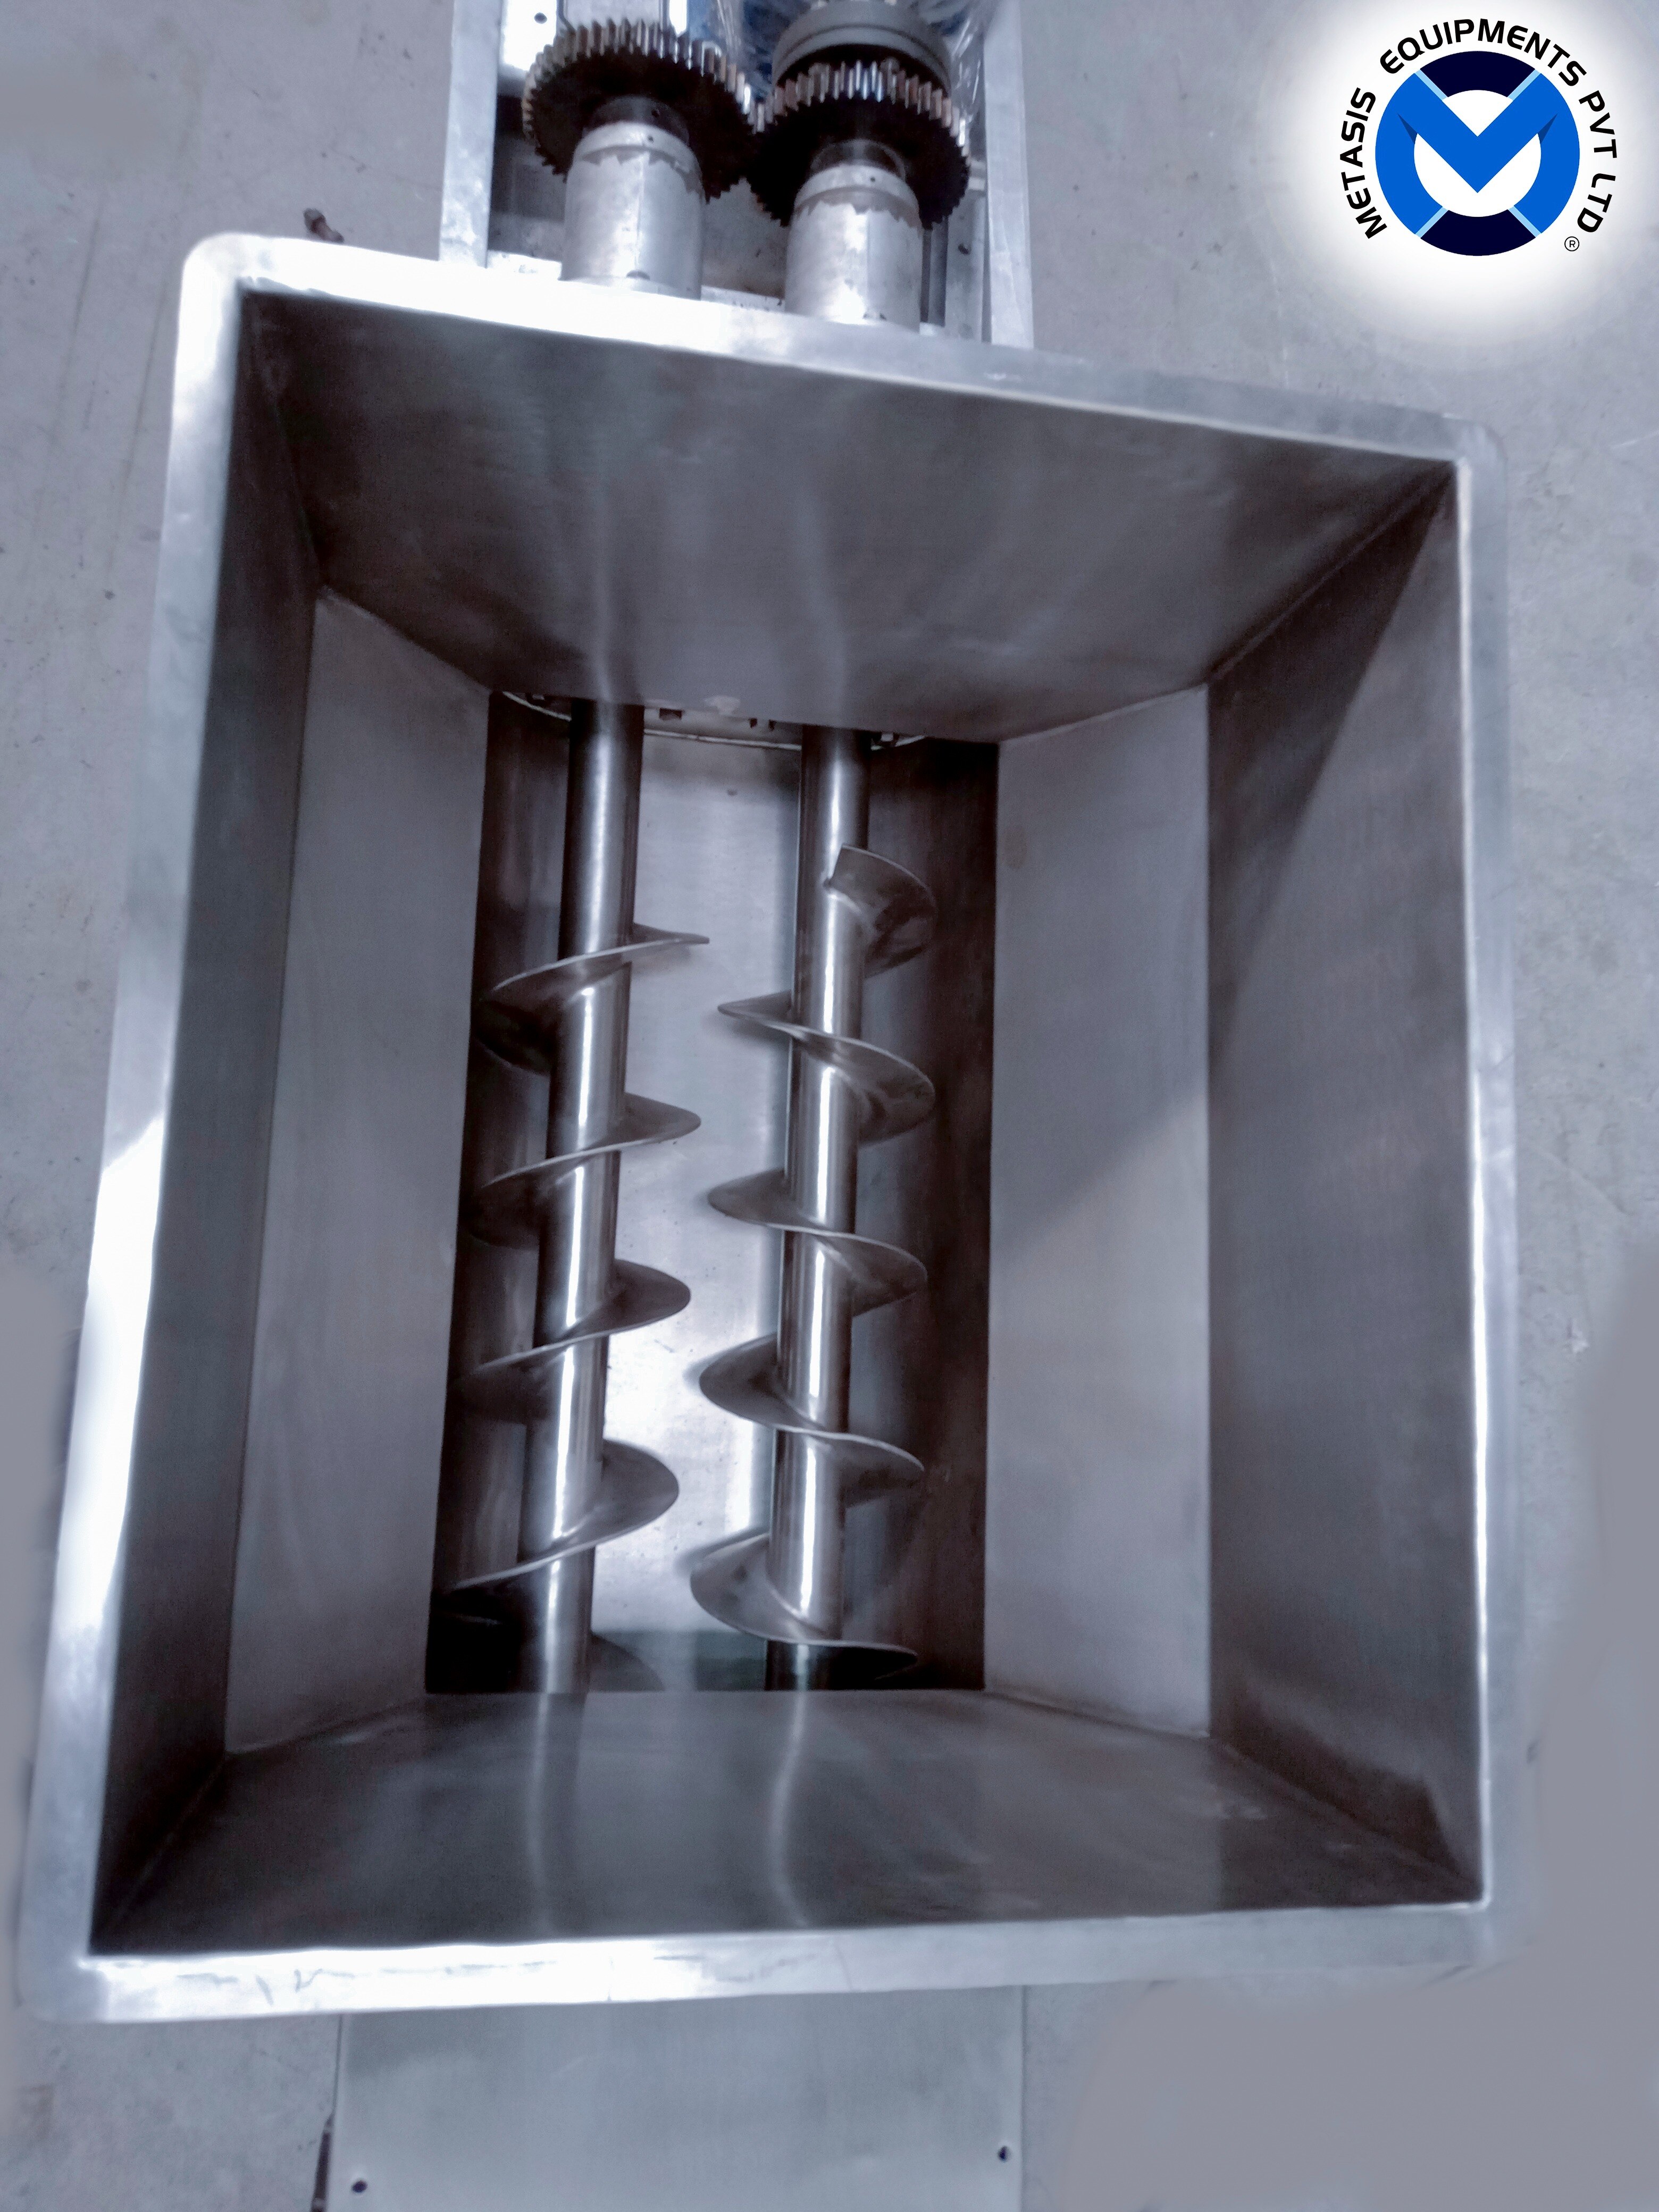
- Inspect the trough, screw flight, shaft, hanger bearings, liners, seals, and access covers for deposits, bent parts, heat marks, wear, and actual shaft-to-trough or shaft-to-liner clearance.
- Inspect the discharge chute, receiving vessel, valve position, vent, and downstream level for a restriction or back-pressure.
- Compare motor current or calculated torque with gearbox noise, torque-limiter trips, shaft deflection, bearing temperature, discharge flow, and upstream hopper level. Trend these signals together, then test one variable at a time.
| Pattern | Likely direction | Evidence to check |
|---|---|---|
| Sudden current or torque rise | Foreign object, feed surge, or downstream restriction | Trip timing, oversized material, valve position, hopper and receiving-vessel levels |
| Gradual current or torque rise | Wear, caking, or increasing friction | Deposits, moisture and temperature change, bearing heat, clearance, flight and liner wear |
This sequence separates process-side screw conveyor blockage problems from a mechanical jam without creating a second failure.
Trace the blockage to feed, geometry, or mechanical condition
Recurring blockages usually originate in feed rate, conveyor geometry, or mechanical damage—not motor size. Confirm the machine is a conveyor, which transfers material already metered into its inlet, rather than a feeder, which withdraws material uniformly from a hopper and often needs variable pitch, progressive filling, or mass-flow geometry.
Flooding a conveyor with a rotary valve or upstream feeder can pack the trough and sharply raise starting torque.
Check these conditions at the blockage location:
- Verify screw rotation, feed rate, inlet spacing, trough loading, outlet geometry, and whether material enters before startup.
- Do not reuse horizontal capacity calculations for an inclined conveyor; allowable loading and conveying efficiency fall as angle increases.
- Inspect for a plugged outlet, foreign object, inadequate clearance, worn or bent flights, damaged hanger bearing, and product accumulated around a support.
- Record shaft-to-trough or shaft-to-liner clearance, bearing temperature, gearbox noise, shaft deflection, motor current, torque-limiter trips, discharge flow, and upstream hopper level.
Compare the design choices that can determine whether the problem returns:
| Option | What to compare | Blockage risk to investigate |
|---|---|---|
| Shafted or shaftless | Hanger arrangement and product contact | Deposits around supports versus liner friction |
| Diameter and pitch | Capacity, speed, and trough loading | Overfeeding, compaction, or low conveying efficiency |
| Trough and liner | Shape, material, wear, and flight thickness | Reduced clearance, adhesion, or abrasive wear |
A screw conveyor manufacturer should also define whether the system must restart loaded. If it must, specify torque limiting, shear protection, current limits, and a control sequence that unloads or purges the screw before restart when possible.
Check whether the material changes inside the conveyor
Do not label a blockage a screw failure until you know whether the material at the jam differs from the feed. Cooling can crystallize or solidify a product; heating can soften it and make it adhere. Residence time can permit curing, reaction, agglomeration, or moisture pickup.
Give the investigator a material-data sheet containing:
- Bulk density, particle-size distribution, moisture percentage, flowability, angle of repose, temperature, abrasiveness, corrosiveness, stickiness, feed rate, required capacity, and operating hours.
- For chemical service, add pH, chemical composition, SDS-based handling controls, and any combustible-dust or flammable-vapour classification.
- Compare inlet and outlet samples with material recovered at the blockage location. Record whether the product compacts under pressure, cakes, melts, reacts, or degrades under shear.
| Material condition | What it indicates | Design response |
|---|---|---|
| Compacts under pressure | The screw can densify its own load | Consider a feeder or different conveying method |
| Highly abrasive | Flight and trough clearance will increase | Specify a replaceable liner and wear strategy |
| Fragile or shear-sensitive | Speed and flight action can damage particles | Reduce shear or select another conveyor |
| Residence-time sensitive | Product can build up, cure, or react | Shorten residence time, add purge, heating, or insulation |
For a chemical plant screw conveyor in Pimpri Chinchwad, review product-contact metals, seals, vent connections, washdown compatibility, static control, and hazardous-area classification. These findings can justify shaftless construction, heat tracing, insulation, or a different conveying method instead of a larger motor.
Ask for a revised design basis and blockage acceptance test
After evidence confirms a recurring failure, require an investigation report and revised design basis, not only a replacement quotation. A screw conveyor manufacturer for repeated blockages in Pimpri Chinchwad must show what caused the stoppage and how the proposed design prevents it.
1. Send the manufacturer the blockage frequency, trip history, cleaning method, photographs of deposits, inlet and discharge drawings, inclination, batch or continuous duty, duty cycle, actual moisture, temperature, bulk density, particle size, and the required loaded-restart condition.
2. Require calculations and explanations for the selected diameter, pitch, speed, trough loading, inlet arrangement, outlet size, liner, flight thickness, bearing layout, drive torque, and protection devices. The report must address feed surges, discharge back-pressure, caking, clearances, and whether the failure is process-side or mechanical.
3. Put the acceptance test in writing. Specify continuous run time without plugging, throughput at the actual material moisture and temperature, maximum motor current or calculated torque, loaded-restart performance, leakage or dust limits, and access for inspection and cleaning. Nameplate capacity alone proves little.
4. For a chemical plant screw conveyor in Pimpri Chinchwad, include product-contact materials, seals, vent connections, washdown compatibility, static control, corrosion resistance, and combustible-dust or flammable-vapour controls.
Metasis Equipments Pvt Ltd is relevant when the review must cover the screw, feeder, discharge, controls, and containment as one system. Compare proposals by measured blockage resistance, not by motor size or empty-running capacity.
Related product
 | Screw Conveyor Global Leader in Custom Screw Conveyor Solutions Metasis Equipments Pvt. Ltd. View product → |
Frequently asked questions
When should repeated screw conveyor blockages trigger an investigation?
Treat two stoppages within 30 days or 100 operating hours as repeated blockage. Escalate any event that requires opening the trough to remove compacted material.
What evidence should you collect before changing a screw conveyor?
Record the blockage location, feed rate, material condition, torque or motor load, operating sequence, and the condition of the screw, trough, inlet, and discharge.
How can you distinguish feed, geometry, and mechanical causes?
Compare events against feed surges and material changes, inspect inlet and discharge geometry, and check for worn flights, shaft misalignment, buildup, damaged liners, or drive problems.
What should a revised screw conveyor design basis and acceptance test include?
Define material properties, bulk density, moisture, temperature, capacity, speed, duty cycle, inlet and discharge conditions, and a blockage-free operating test under representative loads.