
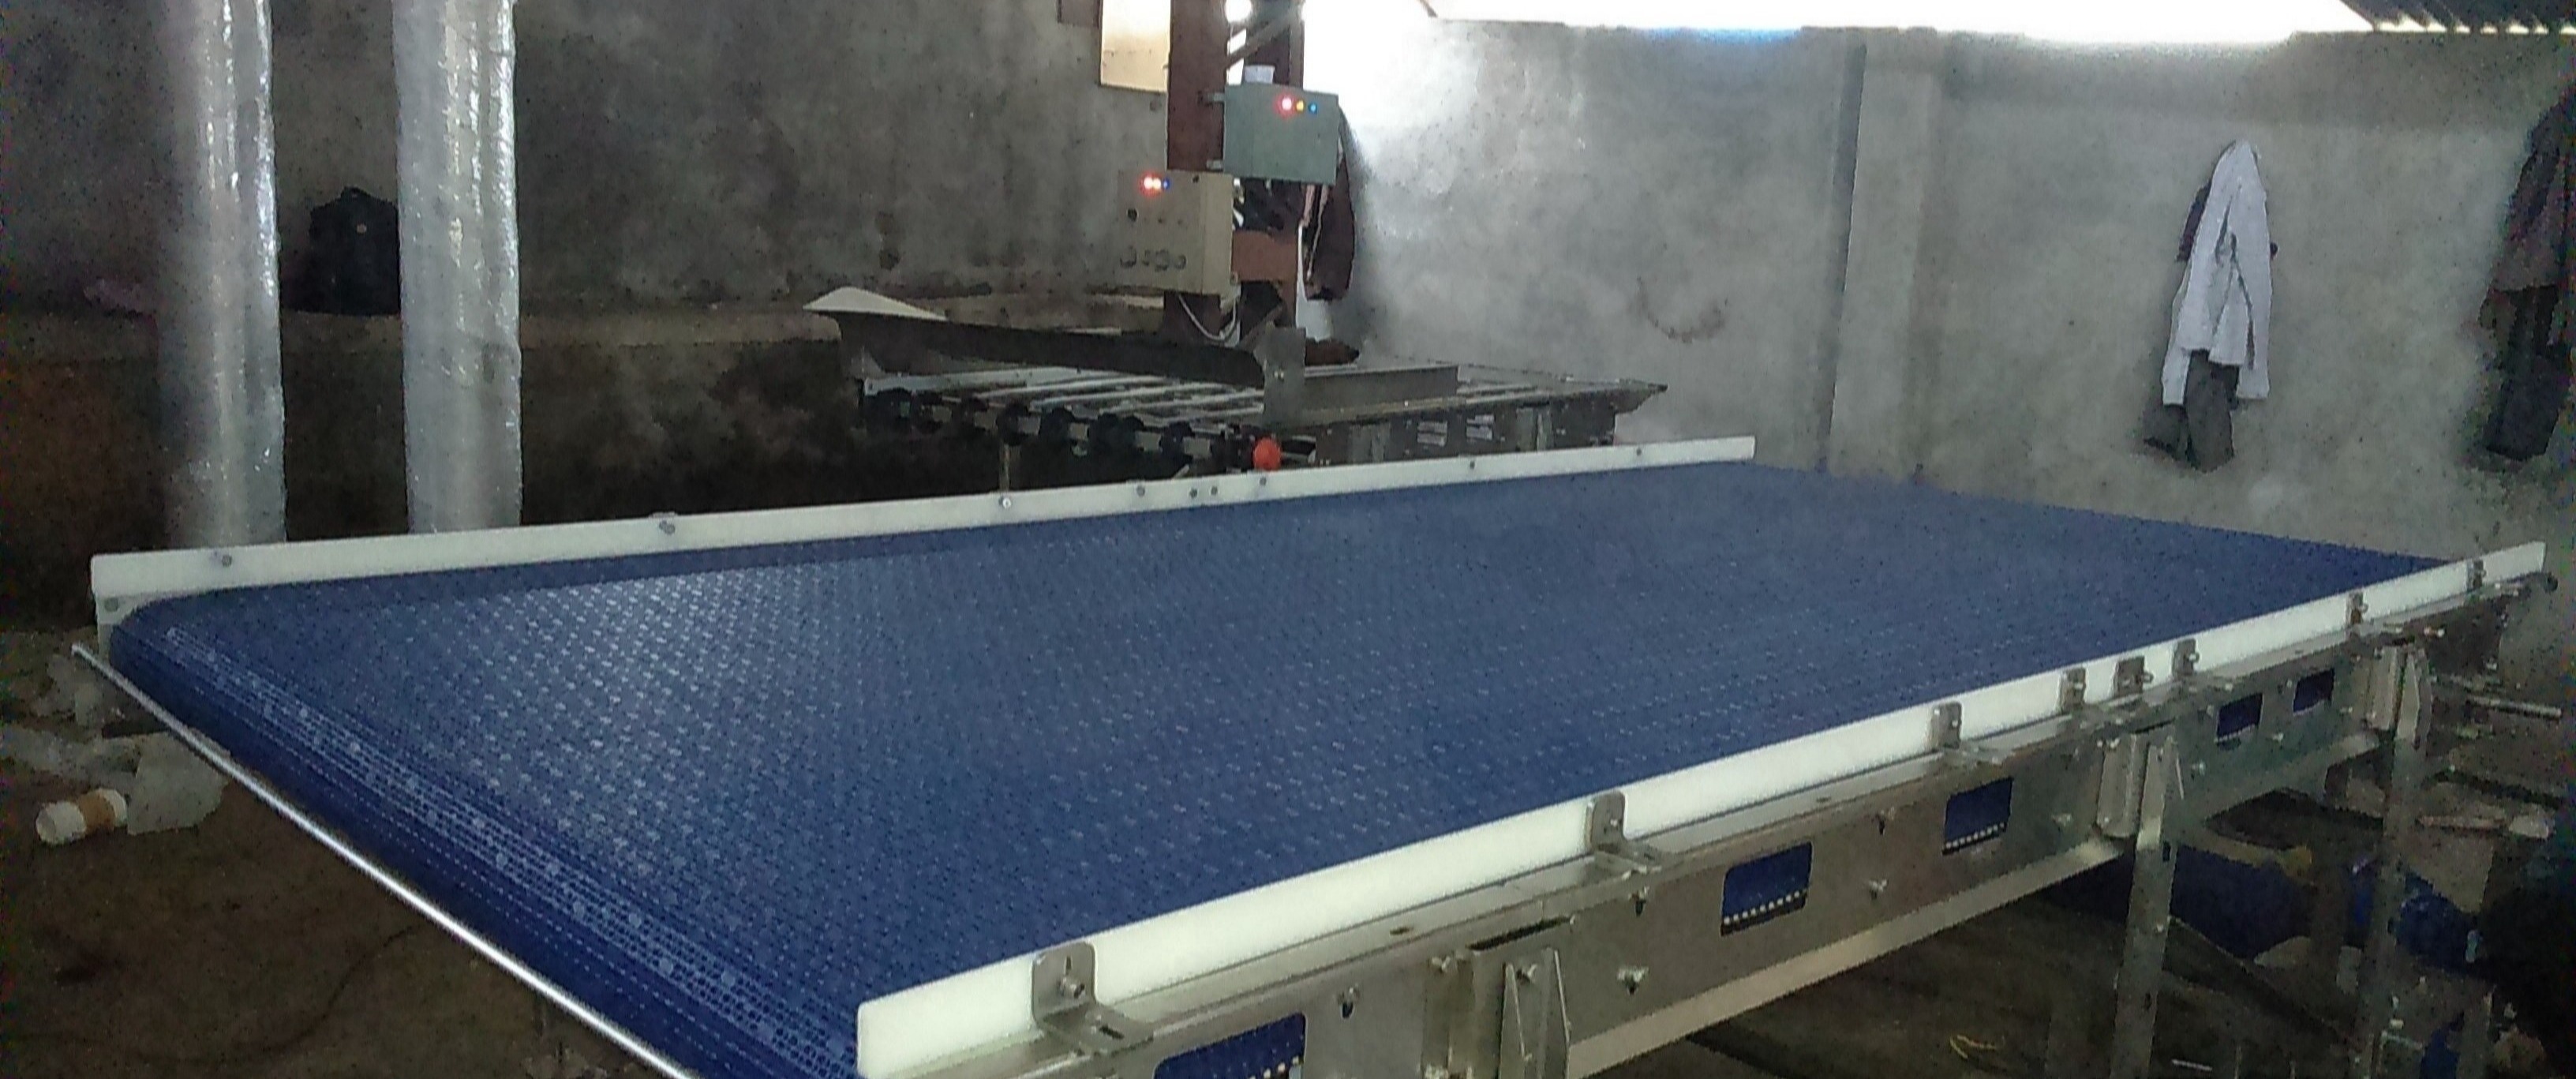
Material movement is an essential part of industrial operations. Manufacturing facilities dealing with bulk materials require reliable transportation systems to move products efficiently between different production stages.
A belt conveyor manufacturer designs and develops conveyor systems according to application requirements such as material type, load capacity, distance, operating environment, and production speed.
Belt conveyors are widely used in industries including mining, food processing, chemical manufacturing, agriculture, and general engineering because they provide continuous material movement with reduced manual handling.
Understanding Belt Conveyor Applications
A belt conveyor system consists of a continuous belt that moves materials from one location to another. The design varies depending on the application.
Common uses include:
Transporting raw materials
Moving finished products
Feeding processing equipment
Connecting different production areas
Handling bulk materials
The right conveyor design depends on factors such as:
Material weight
Particle size
Moisture level
Required speed
Conveyor length
Inclination angle
Selecting The Right Conveyor Design
Different industries require different conveyor solutions.
For example:
Food Belt Conveyor
Food processing applications require hygienic designs suitable for handling food products and powders.
Sand Belt Conveyor
Construction and mineral industries often require durable systems capable of handling abrasive materials.
Iron Ore Belt Conveyor
Mining applications require heavy-duty conveyor systems designed for high loads and continuous operation.
Biomass Belt Conveyor
Agricultural industries require solutions suitable for handling biomass materials with varying moisture content.
Benefits Of Industrial Belt Conveyors
A properly designed conveyor system helps industries achieve:
Reduced manual material handling
Improved production flow
Better workplace safety
Consistent material transfer
Increased operational efficiency
For industries operating in Pimpri-Chinchwad, Maharashtra, efficient material handling is important because manufacturing facilities often require smooth movement of materials across different production stages.
Importance Of Choosing An Experienced Manufacturer
A conveyor system should be designed according to actual operational requirements rather than selecting a standard model without evaluation.
Businesses should consider:
Material characteristics
Production capacity
Installation environment
Maintenance requirements
Expansion possibilities
Metasis Equipments Pvt Ltd develops industrial equipment solutions by considering application-specific requirements and process integration.
Improving Industrial Workflow Through Conveyor Systems
A well-planned conveyor installation supports better production coordination. It reduces unnecessary movement, improves process continuity, and helps industries maintain consistent operations.
Before selecting a belt conveyor manufacturer, companies should evaluate technical capability, engineering approach, and experience with similar applications.
For manufacturing industries in Pimpri-Chinchwad looking to improve material handling efficiency, a properly engineered belt conveyor system can support smoother and more reliable production processes.