
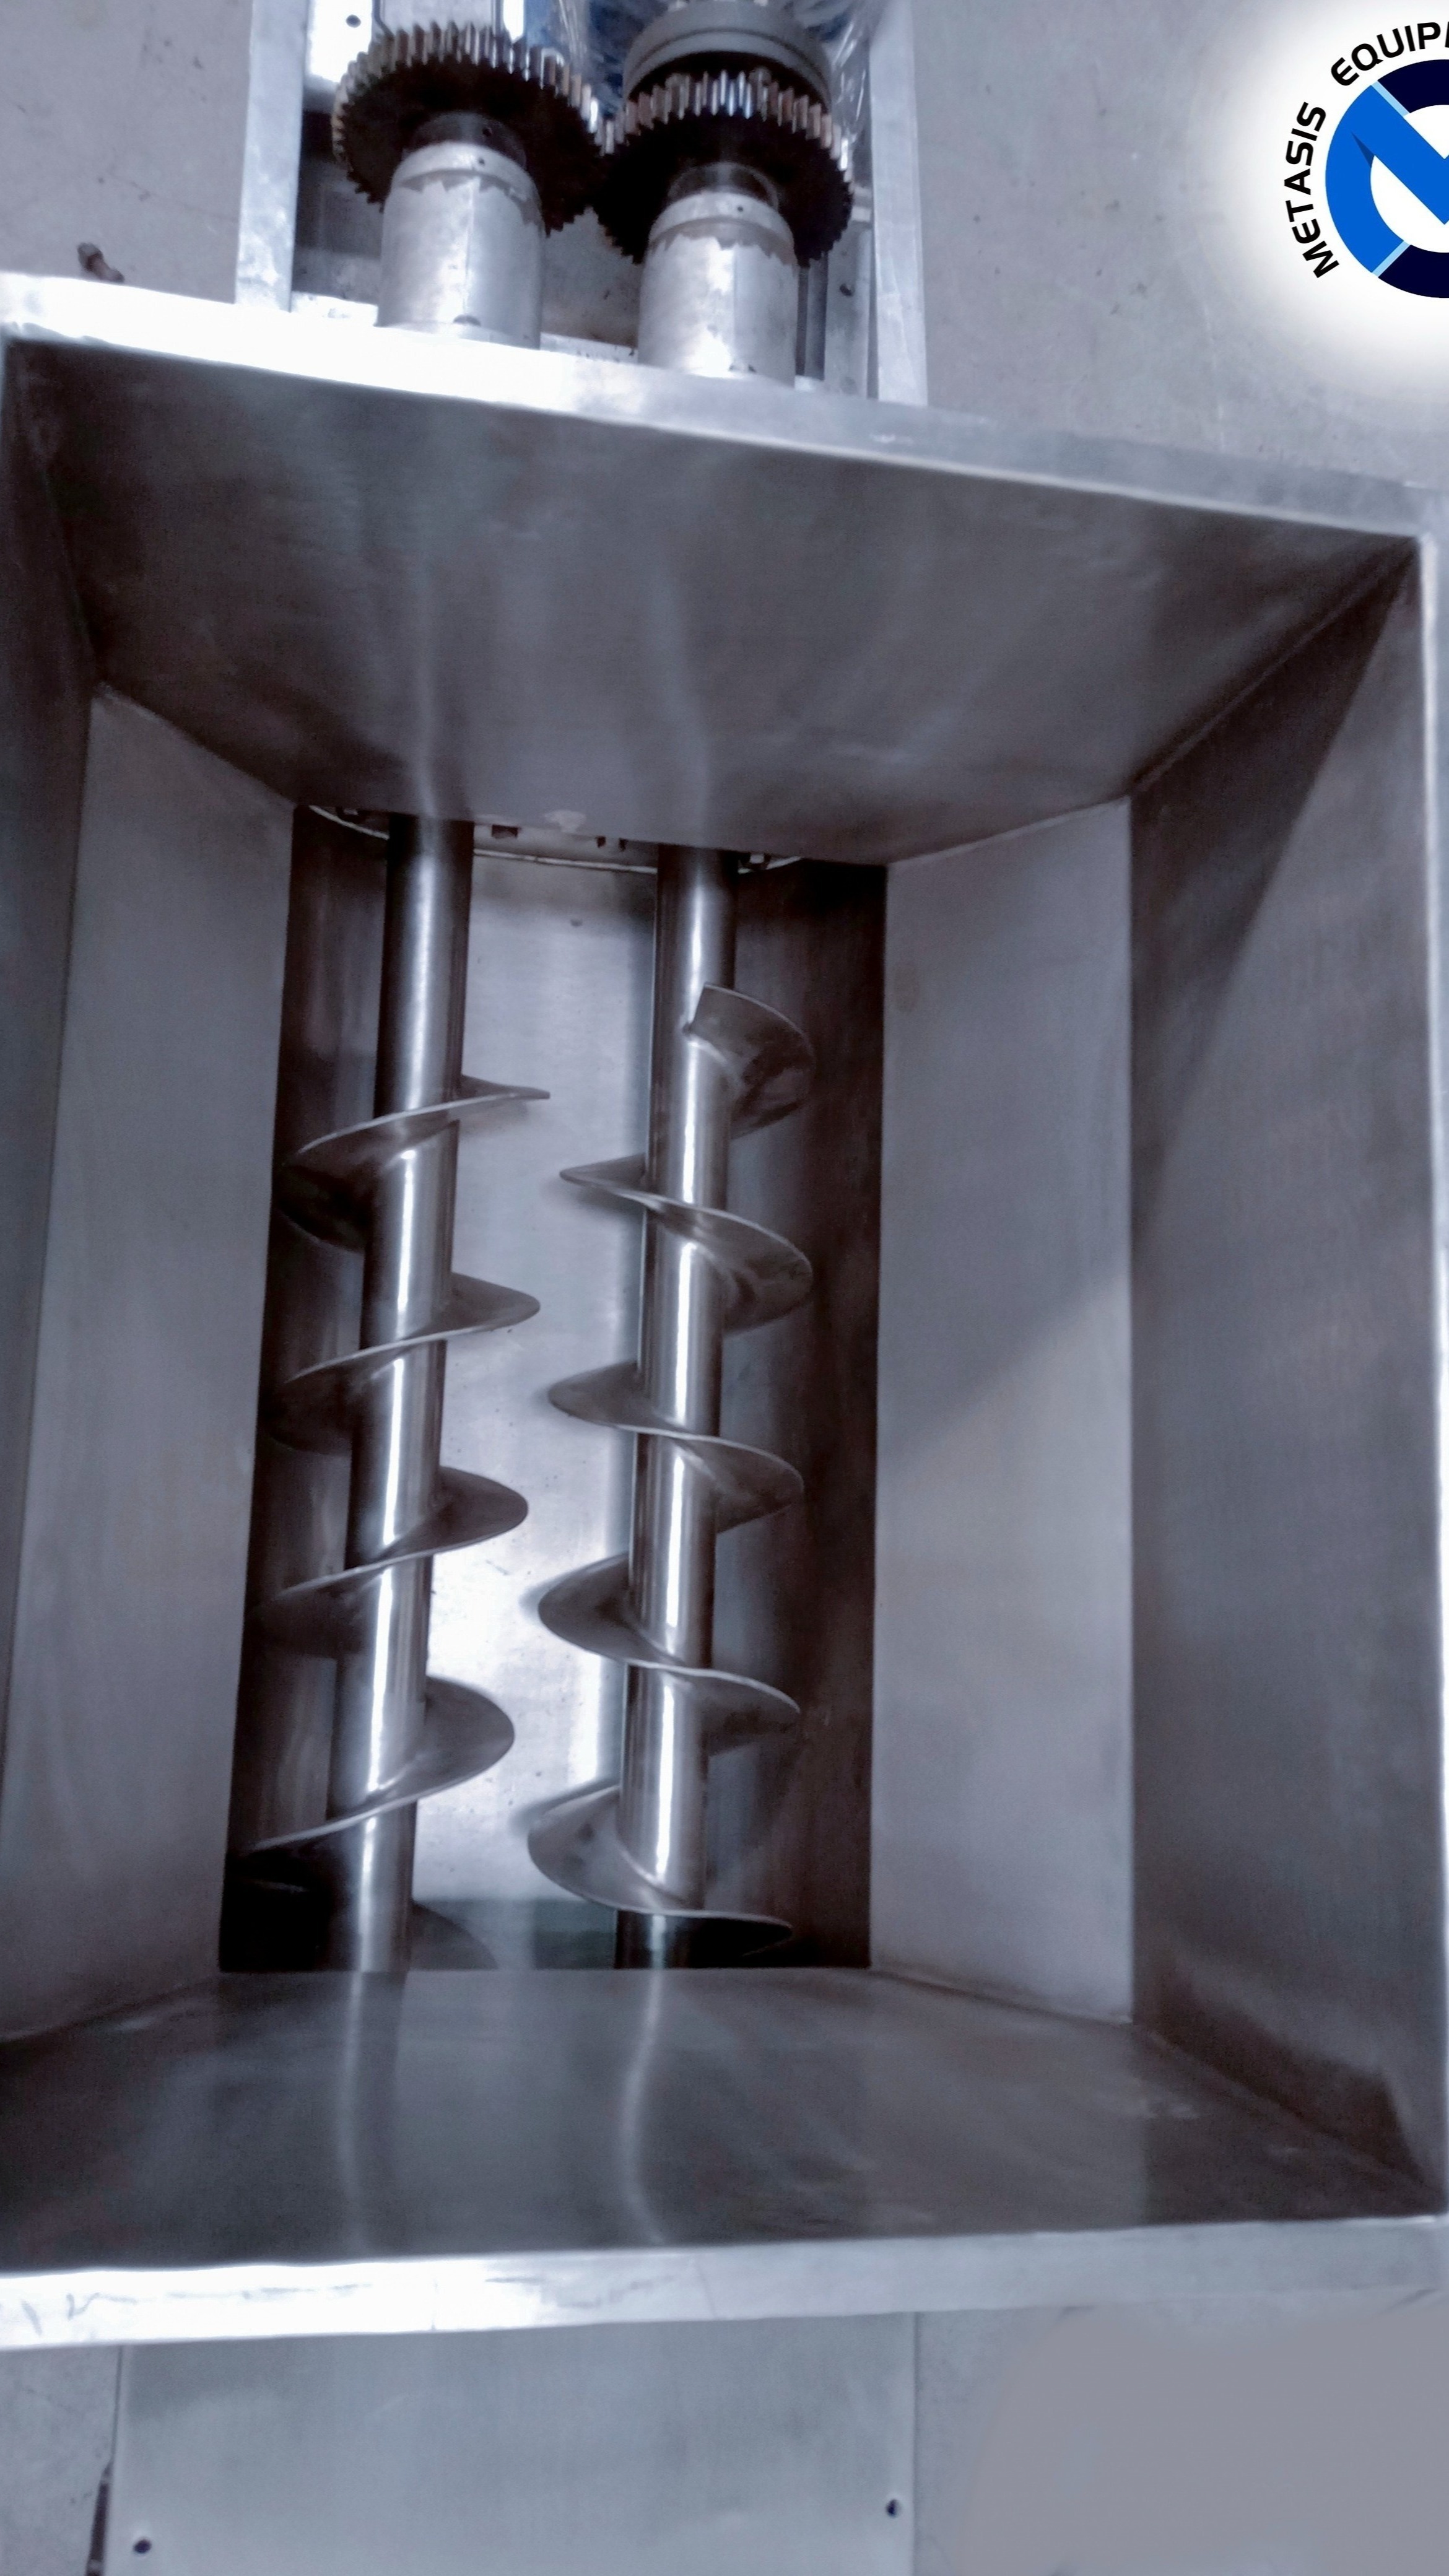
Efficient movement of powders, granules, and semi-solid materials is essential for smooth industrial production. Many industries require controlled transportation systems that can move materials through horizontal, inclined, or vertical pathways while maintaining process consistency.
A screw conveyor manufacturer from India designs equipment that helps industries handle different materials across applications such as food processing, pharmaceuticals, chemicals, agriculture, and manufacturing.
Screw conveyors are widely used because they provide enclosed material transfer, require limited space, and can be customized according to production requirements.
Understanding Screw Conveyor Systems
A screw conveyor uses a rotating helical screw blade inside a tube or trough to move materials from one point to another. The movement depends on screw design, rotation speed, material characteristics, and conveyor configuration.
Different applications require different types of screw conveyor solutions, including:
Horizontal screw conveyors
Inclined screw conveyors
Vertical screw conveyors
Flexible screw conveyors
Specialized industrial screw conveyors
Each design serves a specific material handling requirement.
Applications Of Screw Conveyors In Industries
Screw conveyors are used in multiple sectors because of their adaptability.
Food Processing Industry
Food manufacturers use screw conveyors for transporting powders, grains, and ingredients while maintaining controlled movement.
Pharmaceutical Industry
Pharmaceutical production requires careful handling of powders and sensitive materials. Suitable screw conveyor systems help maintain process efficiency.
Chemical Industry
Chemical plants use screw conveyors for transferring powders and bulk materials where enclosed movement is preferred.
Agricultural And Biomass Applications
Materials such as biomass, agricultural waste, and processed products require customized conveyor designs based on moisture and density.
Selecting The Right Screw Conveyor Design
The correct conveyor selection depends on several factors:
Material type
Particle size
Flow characteristics
Required capacity
Transfer distance
Inclination requirement
Temperature conditions
For example, a screw conveyor for food powder may require different construction compared to a coal screw conveyor or biomass screw conveyor.
Industries should evaluate these factors before finalizing equipment specifications.
Screw Conveyor Solutions For Different Materials
Specialized systems are developed for different applications, including:
Screw conveyor for semisolid materials
Screw conveyor for pharma powder
Screw conveyor for food powder
Biomass screw conveyor
Coal screw conveyor
The design must ensure smooth material movement while reducing issues such as blockages, spillage, and inconsistent flow.
Importance Of Engineering-Based Conveyor Design
A conveyor system is not just a transportation device. It is an important part of the complete production process.
Poorly designed material handling systems can affect:
Production efficiency
Equipment coordination
Maintenance schedules
Operating costs
Metasis Equipments Pvt Ltd develops industrial handling solutions by considering material properties and process requirements.
For industries in Pimpri-Chinchwad, Maharashtra, selecting a suitable screw conveyor manufacturer helps businesses create reliable material handling systems that support continuous production.
A well-engineered screw conveyor improves workflow, reduces manual handling, and contributes to better industrial process management.